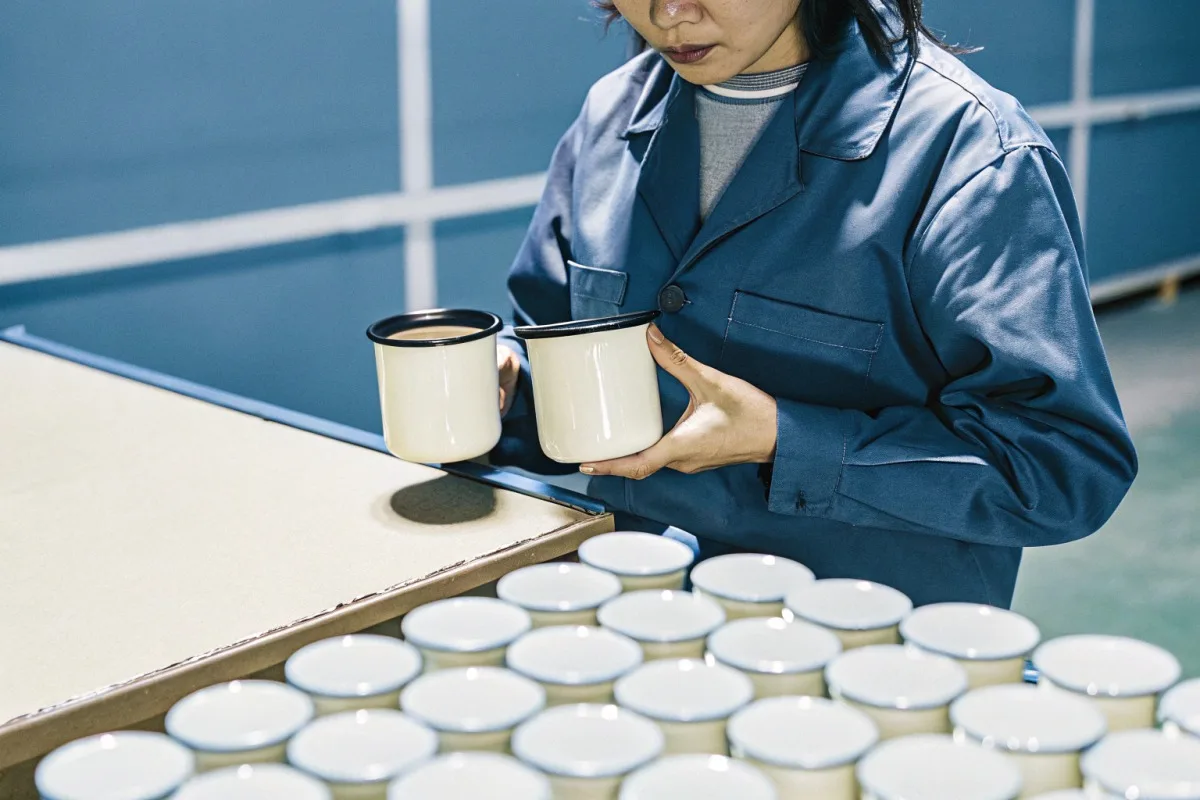
Every week on our production floor in Huizhou, we inspect thousands of enamel mugs before they ship overseas factory audits 1. Surface defects like pinholes and black spots 2 remain the most common quality concern our buyers raise.
Industry standards for pinholes and black spots on enamel mugs vary by manufacturer and region, but reputable suppliers typically allow no more than 3 minor pinholes per mug surface, with black spots not exceeding 1mm in diameter. Hidden defect areas should total less than 7cm² per square meter of enamel surface. These thresholds ensure mugs remain functional, food-safe, and visually acceptable for retail.
Understanding these standards helps you negotiate better quality agreements with suppliers brand reputation 3. Let me walk you through what our quality control teams 4 look for and how you can protect your brand.
How many pinholes and black spots should I accept in my bulk enamel mug order?
When we quote on large orders, buyers always ask about acceptable defect levels. This question matters because it directly impacts your rejection rate and overall costs.
For bulk enamel mug orders, you should accept no more than 2-3 minor pinholes (under 0.5mm) per mug on non-visible areas, and zero visible pinholes on the primary display surface. Black spots should be limited to 1-2 specks under 1mm on secondary surfaces. Any defects larger than these thresholds warrant rejection or reclassification to B-grade stock.
Understanding Defect Categories
Not all defects are equal. Our quality control team classifies them into three levels based on visibility and impact.
| Defect Type | Grade A Standard | Grade B Standard | Rejection Threshold |
|---|---|---|---|
| Micro pinholes (<0.3mm) | Max 2 on hidden areas | Max 5 anywhere | More than 5 total |
| Visible pinholes (0.3-1mm) | Zero allowed | Max 2 on bottom | Any on display surface |
| Small black spots (<1mm) | Max 1 on hidden areas | Max 3 anywhere | Clustered spots |
| Large black spots (>1mm) | Zero allowed | Max 1 on bottom | Any visible location |
Why These Numbers Matter
Our firing kilns 5 operate at temperatures exceeding 850°C. At these temperatures, tiny air bubbles can get trapped in the enamel layer. If the glass powder doesn't flow perfectly, you get pinholes. Black spots often come from furnace scale or contamination during the coating process.
We've found that even the best production runs produce some micro-defects. The goal isn't zero defects—that's unrealistic for hand-finished products. The goal is consistent, predictable quality within agreed limits.
Setting Clear Expectations
Before you place a large order, ask your supplier these questions:
- What is your standard defect acceptance rate per batch?
- Do you offer tiered grading (A-grade, B-grade)?
- How do you handle mugs that fall between grades?
Our contracts typically include a defect rate clause. For example, we guarantee that no more than 3% of units in any shipment will have visible cosmetic defects. Units exceeding this threshold either get replaced or credited.
The Cost Factor
Tighter tolerances mean higher prices. When buyers request zero-defect standards, we increase inspection time and reject more units. This drives up per-unit costs by 15-25%. Most brands find that accepting minor hidden defects keeps costs reasonable without hurting customer satisfaction.
How do I evaluate if the surface defects on my custom mugs meet professional QC requirements?
Our inspection team evaluates over 50,000 mugs monthly. We've developed systematic methods that any buyer can adapt for incoming quality checks.
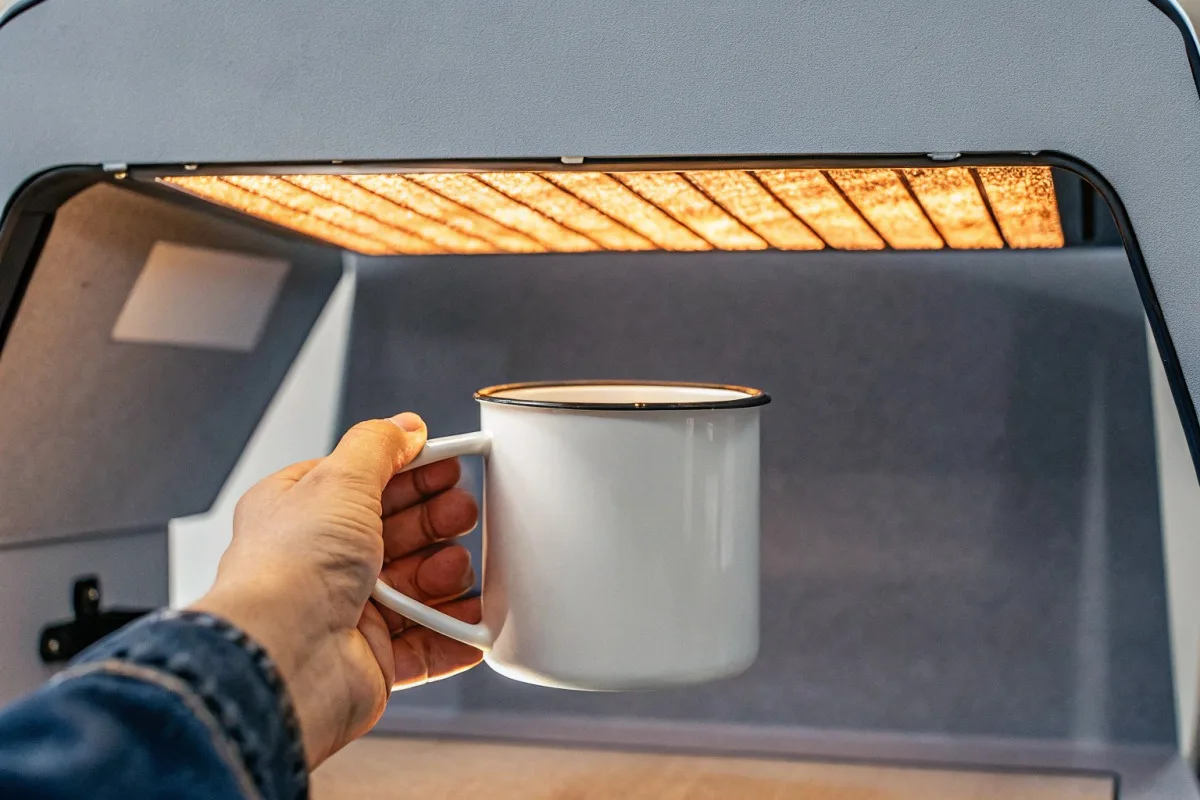
Professional QC evaluation for enamel mug defects requires standardized lighting (5000K daylight), a defined viewing distance (30-45cm), and documented acceptance criteria. Check each mug's exterior, interior, rim, and handle attachment points. Use a magnifying glass for micro-defects. Compare samples against pre-approved golden samples that represent your agreed quality standard.
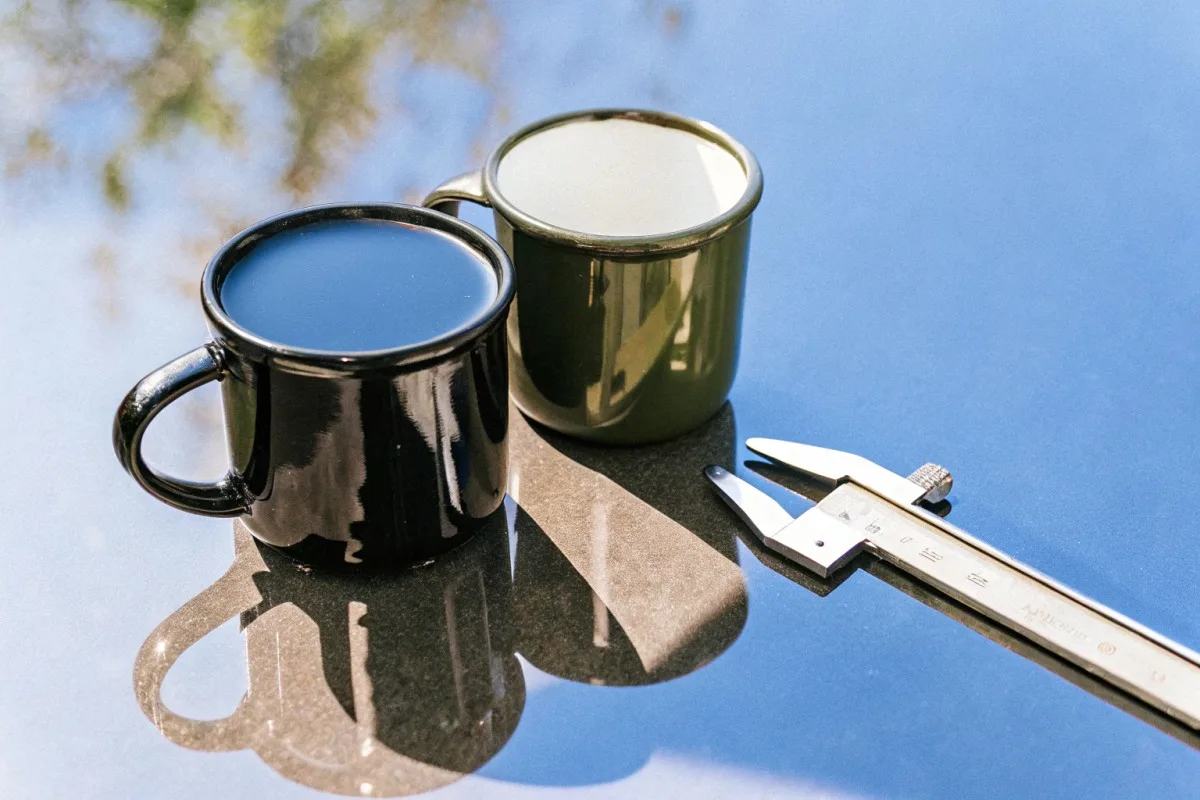
The Inspection Environment
Lighting affects everything. Under warm or dim lighting, small black spots become invisible. Then your customers open boxes under bright retail lights and see every flaw.
| Inspection Factor | Recommended Standard | Why It Matters |
|---|---|---|
| Light source | 5000K LED daylight | Neutral color reveals true defects |
| Light intensity | 800-1000 lux | Shadows show surface irregularities |
| Viewing distance | 30-45cm | Simulates customer first impression |
| Viewing angle | Multiple angles (0°, 45°, 90°) | Catches defects that hide at certain angles |
| Background | Neutral grey or white | Prevents visual interference |
Step-by-Step Evaluation Method
Here's the process our QC inspectors follow:
Step 1: Visual Overview
Hold the mug at arm's length. Rotate it slowly. Look for obvious defects, color inconsistencies, or shape irregularities.
Step 2: Surface Scan
Bring the mug closer. Examine the exterior enamel under direct light. Tilt the mug to catch light at different angles. Pinholes often show as tiny shadows.
Step 3: Interior Check
Look inside the mug. Interior defects affect food safety more than exterior ones. Any exposed metal inside should be flagged immediately.
Step 4: Rim Inspection
The rim receives the most wear. Check for enamel coverage, chips, and rough edges. Black spots often concentrate where the rim dip coating meets the body enamel.
Step 5: Handle Assessment
Examine the handle attachment points. These high-stress areas sometimes show hairline cracks or incomplete enamel coverage.
Using Golden Samples
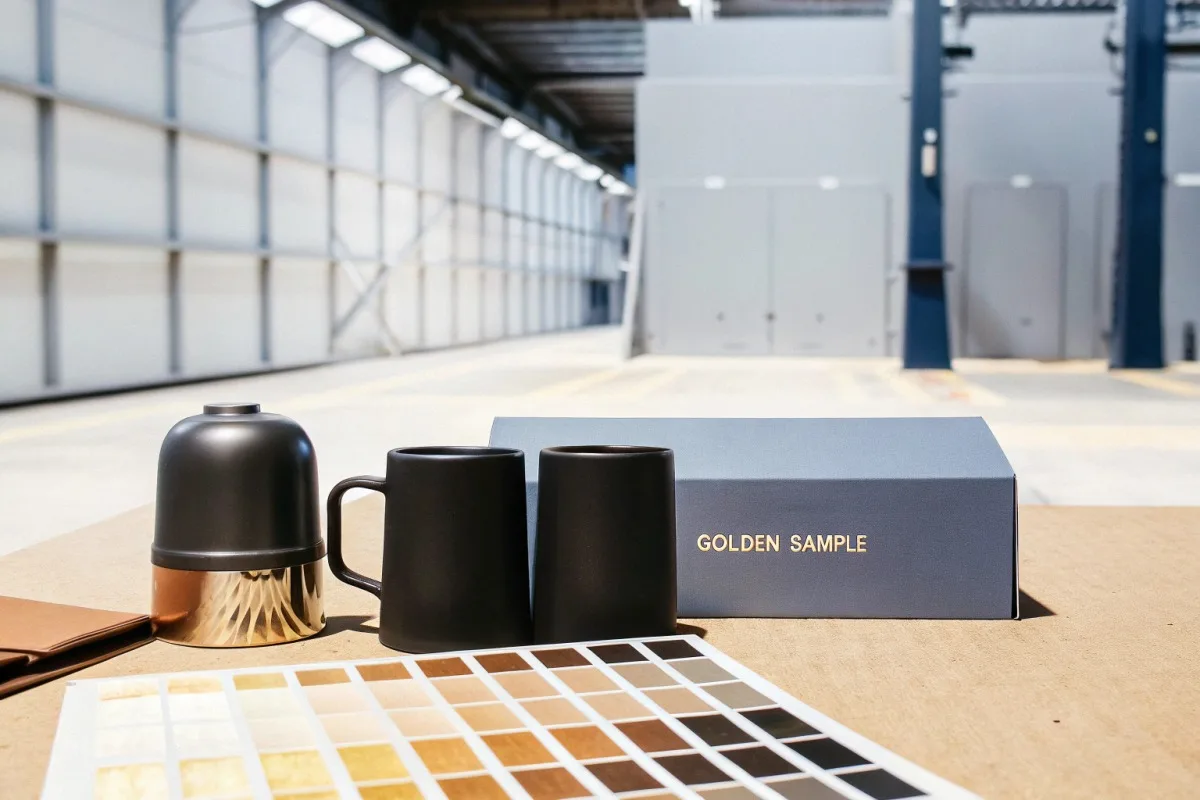
Before production starts, we create golden samples 6 that represent the agreed quality level. These become the reference standard for all inspections. If a mug looks worse than the golden sample, it fails. If it matches or exceeds, it passes.
Always request 3-5 golden samples. Keep one in your office, one with your supplier, and one with any third-party inspection company 7. This prevents disputes about subjective quality judgments.
When to Use Third-Party Inspection
For orders over $10,000 or first-time suppliers, consider hiring a third-party inspection company. Companies like SGS, Bureau Veritas, or Intertek have trained inspectors in major manufacturing regions. They provide unbiased reports with photographic evidence.
What steps can I take to ensure my supplier maintains strict control over black spots during production?
On our production lines, preventing defects costs less than sorting defective products afterward. We've invested heavily in process controls that minimize black spots and pinholes.
To ensure strict black spot control, require your supplier to implement raw material screening, maintain dust-free enamel application environments, control firing temperatures within ±5°C tolerances, and conduct in-line inspections after each production stage. Request process documentation and consider periodic factory audits to verify compliance with agreed procedures.
Root Causes of Black Spots
Understanding causes helps you ask the right questions.
| Cause | Stage | Prevention Method |
|---|---|---|
| Contaminated enamel powder | Raw material | Supplier certification, incoming inspection |
| Furnace scale | Firing | Regular kiln cleaning, temperature control |
| Dust particles | Coating application | Cleanroom environment, air filtration |
| Oxidation | Cooling | Controlled cooling rate, protective atmosphere |
| Handling contamination | Post-firing | Gloves, clean transport containers |
Production Process Controls
Raw Material Verification
Before enamel powder enters our production area, we test samples from each batch. We check for particle size consistency and foreign matter. Contaminated batches get rejected immediately.
Environment Control
Our coating rooms maintain positive air pressure. Filtered air continuously flows outward, preventing dust from entering. Workers wear lint-free clothing and gloves.
Temperature Monitoring
Our kilns have digital temperature controllers with logging capability. We can provide buyers with firing records showing temperature curves for specific production batches. Fluctuations beyond ±5°C trigger automatic alerts.
In-Line Inspection
We inspect mugs at three stages: after the base coat firing, after the color coat application, and before final packing. Problems caught early get corrected. Problems caught late mean wasted materials.
Questions to Ask Your Supplier
Use these questions during supplier evaluation:
- What is your enamel powder sourcing process?
- Do you have a dedicated cleanroom for enamel application?
- Can you provide firing temperature logs for my orders?
- What is your inspection protocol at each production stage?
- How do you train new workers on contamination prevention?
Factory Audit Checklist
If you visit a supplier's factory, check these items:
- Enamel powder stored in sealed, labeled containers
- Coating area separated from metalworking area
- Workers wearing appropriate protective clothing
- Kilns equipped with temperature monitoring displays
- Inspection stations with adequate lighting
- Defective product segregation area clearly marked
Suppliers who welcome audits typically have better quality systems than those who resist.
How do these common enamel imperfections affect the resale value and brand reputation of my private-label mugs?
We've seen how quality issues ripple through supply chains. One bad batch can damage years of brand building. Here's what our buyers have taught us about market impact.
Enamel imperfections directly impact your brand reputation and profit margins. Visible pinholes and black spots increase return rates by 15-25%, trigger negative reviews, and can downgrade your products from premium to discount positioning. For private-label brands, consistent quality builds customer trust; visible defects suggest poor supplier management and erode perceived value.
The True Cost of Defects
Direct costs are obvious: returns, replacements, shipping. Hidden costs hurt more.
| Cost Category | Low Defect Rate (<2%) | Moderate Defect Rate (5-8%) | High Defect Rate (>10%) |
|---|---|---|---|
| Return rate | 1-2% | 5-8% | 15-25% |
| Negative reviews | Rare | Occasional | Frequent |
| Repeat purchase rate | High (60%+) | Moderate (40%) | Low (<25%) |
| Customer service hours | Minimal | Moderate | Significant |
| Brand perception | Premium | Standard | Discount |
Customer Expectations by Market Segment
Different markets tolerate different defect levels.
Premium/Gift Market
Customers paying $25+ for a single mug expect perfection. Even tiny visible defects trigger returns and complaints. These buyers read reviews carefully before purchasing.
Outdoor/Camping Market
Customers understand that enamel products have a rugged, handmade character. Minor imperfections add authenticity. However, defects suggesting poor durability (exposed metal, thin spots) still generate complaints.
Promotional Products Market
Corporate buyers ordering branded mugs for events care more about logo accuracy than minor surface imperfections. They may accept B-grade products at lower prices. However, they still reject obvious quality issues that reflect poorly on their brand.
Protecting Your Brand
Clear Product Descriptions
Set accurate expectations. If you sell handmade-style mugs, mention that minor variations are normal. This reduces complaints from customers expecting factory-perfect products.
Quality Guarantees
Offer easy returns for quality issues. This sounds expensive, but it builds customer confidence and encourages purchases. Most customers never return products; they just need to know they can.
Supplier Accountability
Include quality clauses in your supplier agreements. Define defect thresholds, inspection methods, and remedies for non-compliance. This creates shared accountability.
Long-Term Brand Building
We've worked with brands that started with budget products and gradually upgraded quality. They raised prices slowly as their reputation improved. Within three years, they moved from competing on price to competing on brand loyalty.
The opposite path is painful. Brands that cut corners on quality to save costs often watch their market position erode. Negative reviews compound. Each new customer reads old complaints. Recovery takes years.
Invest in quality agreements upfront. The money you spend on better inspection and tighter standards pays dividends in customer loyalty and brand equity.
Conclusion
Understanding pinhole and black spot standards helps you negotiate better supplier agreements and protect your brand. Set clear thresholds, inspect systematically, and choose suppliers who share your quality commitment.
Footnotes
1. Details the purpose and benefits of conducting factory audits for quality and compliance. ↩︎
2. Explains common defects like pinholes and black spots in enamel cast iron cookware. ↩︎
3. Discusses how product quality and quality control directly influence a brand’s reputation. ↩︎
4. Defines the role and importance of quality control in manufacturing processes. ↩︎
5. Provides information on different firing methods and types of kilns used in ceramic production. ↩︎
6. Describes the concept and importance of golden samples in manufacturing quality control. ↩︎
7. SGS is a leading global inspection company, and their inspection services page provides authoritative information on what a third-party inspection company does. ↩︎